Engineered for high-altitude cold protection, rapid moisture evaporation, and ergonomic compression.
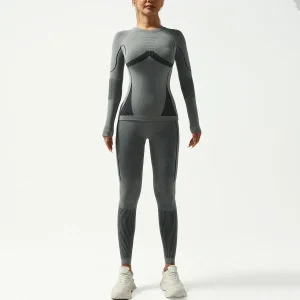
The global functional apparel market is undergoing a seismic shift toward intelligent micro-climate regulation. Modern base layer garments are no longer viewed merely as passive insulation; they are active thermodynamic systems designed to manage moisture vapor transmission, maintain core muscle homeostasis, and prevent metabolic fatigue during extreme environmental exposure.
In regions serving maritime hubs, tactical commercial sectors, and outdoor sports ecosystems—such as the expanding commercial footprint across Grenville—demand for versatile, multi-climate thermal base layers has increased by over 18.4% year-over-year. B2B buyers and brand importers servicing the Grenville regional market require high-density, low-weight fabrics capable of transitioning seamlessly between high-humidity maritime work conditions and low-temperature expedition environments.
Rigorously tested under ISO 11092 and ASTM D1518 thermal resistance protocols.
The science behind next-generation thermal retention and moisture transport systems engineered by Guangzhou Lifted Clothe Co., Ltd.
Utilizing ultrafine merino fibers sourced from certified sustainable farms. Merino wool creates microscopic air pockets that lock in radiant body heat while possessing natural keratine fibers that absorb up to 35% of their weight in moisture before feeling wet, delivering unparalleled temperature regulation in variable climates.
Engineered for continuous sweat transport. Inner face synthetic filaments feature a 3D channel matrix that pushes liquid moisture outwards toward the micro-porous outer fabric layer, evaporating sweat 3x faster than standard cotton base layers, preventing post-exercise hypothermia.
Designed for extreme durability and zero internal skin friction. Our seamless circular knitting machines and ultra-flat structural seams ensure maximum elasticity under multidirectional strain, allowing complete freedom of movement during high-intensity training or heavy physical labor.
| Fabric Technology Category | Composition Ratio | Fabric Weight (GSM) | Primary Thermal Application | Moisture Management Level |
|---|---|---|---|---|
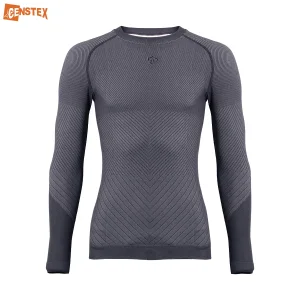
| Pure Merino Workwear Thermal | 100% Fine Australian Merino Wool | 200 - 260 GSM | Outdoor Expedition, Workwear & Cold Weather Marine | Natural Hydrophilic Vapour Management |
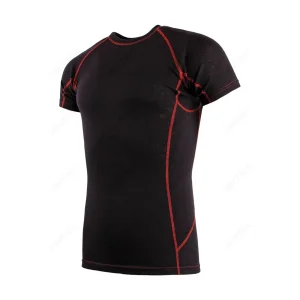
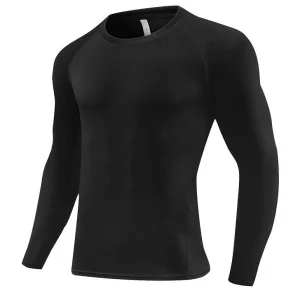
| Seamless Sport Compression | 85% Polyester / 15% Elastane Seamless Knit | 180 - 220 GSM | High-Intensity Athletic Training, Skiing, Running | Accelerated Quick-Dry Channeling (Push-Pull) |
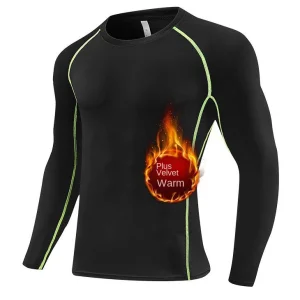
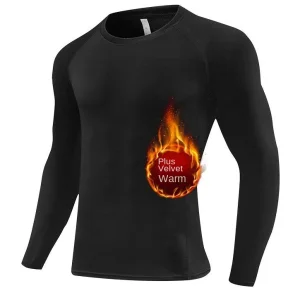
| Plush Fleece Brushed Base Layer | 92% Micro-Polyester / 8% Spandex Fleece | 240 - 300 GSM | Sub-Zero Winter Outdoor & Heavy Duty Protection | High Thermal Insulation (CLO > 0.90) |
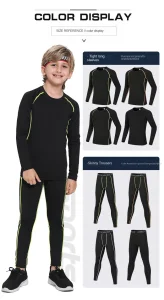
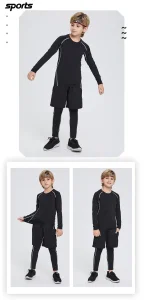
| Youth & Kids Active Compression | 88% Poly-Nylon / 12% Spandex Blend | 160 - 190 GSM | All-Season Youth Sports, Basketball, Football | Ultra-Fast Evaporation & Chafing Defense |
Why leading global brands and importers serving the Grenville market partner with Guangzhou Lifted Clothe Co., Ltd.
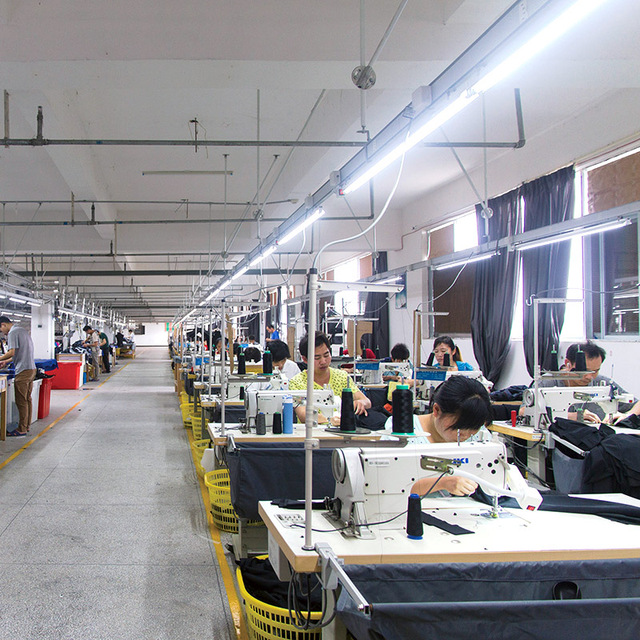
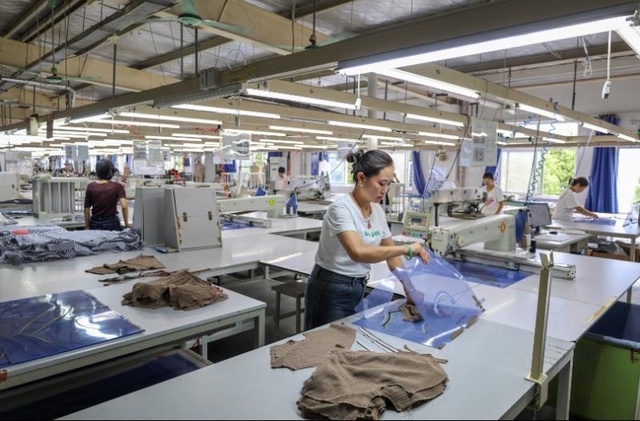
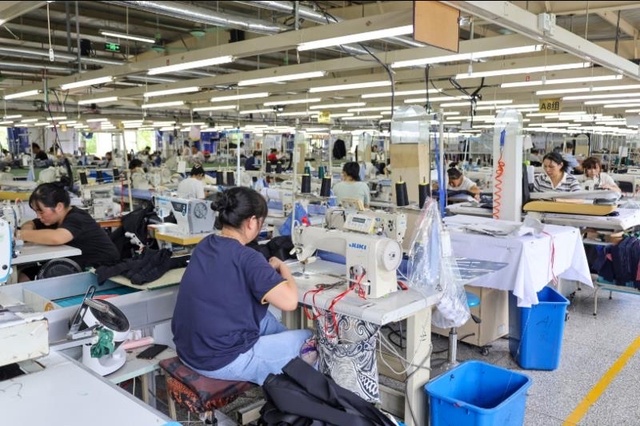
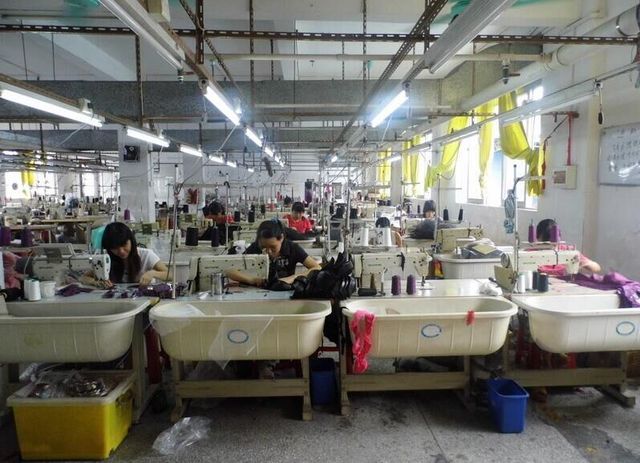
Located in the apparel manufacturing capital of Guangzhou, China, we possess direct vertical integration spanning thread spinning, custom fabric dyeing, 3D computerized knitting (Shima Seiki & Santoni systems), automated pattern cutting, and automated QA packing lines. This drastically eliminates intermediary markups and reduces production lead times.
Every batch of base layer thermal wear undergoes stringent testing for color fastness, dimensional stability after washing, pilling resistance (Grade 4.5+), and stretch recovery. Our facilities adhere strictly to ISO9001 quality management systems and OEKO-TEX Standard 100 non-toxic human ecology requirements.
We provide full-spectrum customization services tailored for distributors supplying Grenville and international markets. From custom Jacquard logo elastic waistbands, reflective heat-seal transfers, custom tech pack development, to eco-friendly retail packaging, we realize your brand vision seamlessly.
Pioneering high-performance outdoor and thermal garment engineering for global export markets.
Guangzhou Lifted Clothe Co., Ltd. is a professional outdoor apparel manufacturer specializing in the design, development, and production of high-quality clothing for global markets. With a strong focus on functionality, comfort, and performance, the company offers a wide range of products including down jackets, padded jackets, ski wear, swimwear, and yoga apparel.
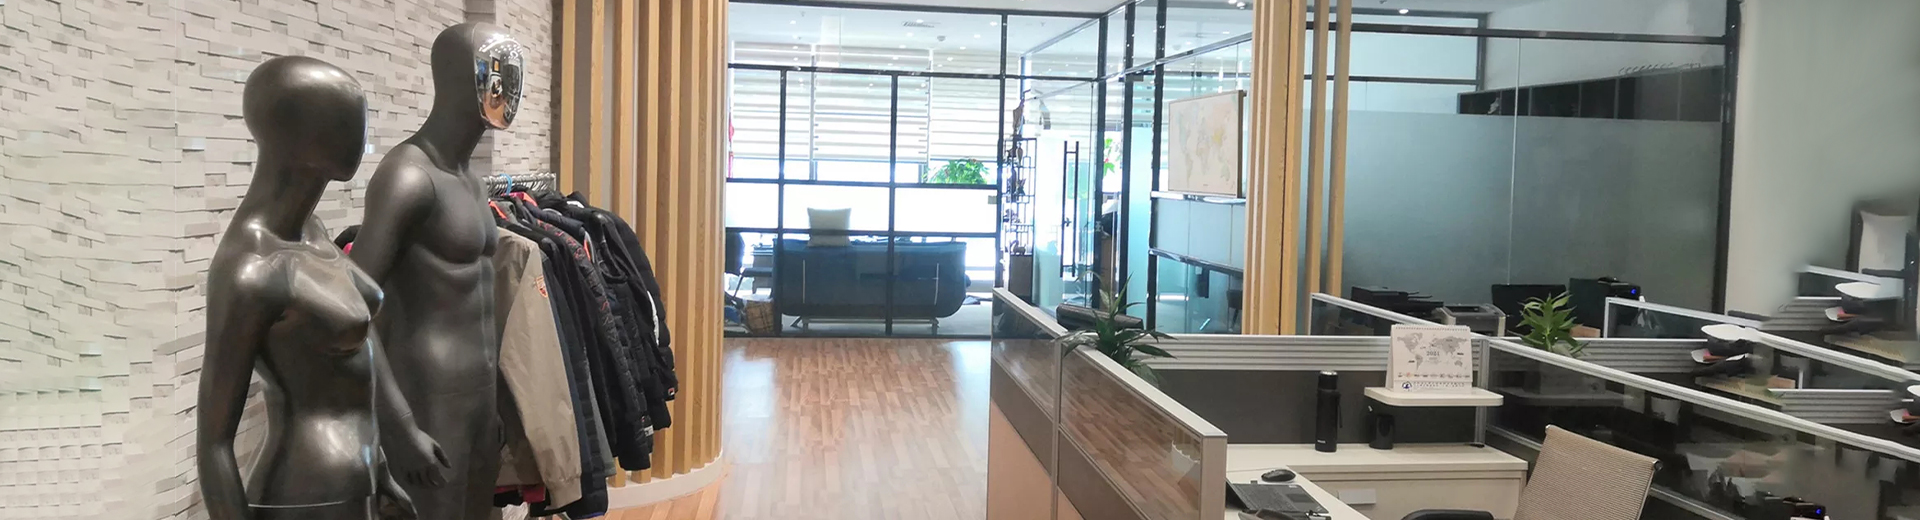
Backed by advanced production facilities and an experienced R&D team, Lifted Clothe is committed to integrating innovative fabric technologies with modern manufacturing processes. Our products are designed to meet the demands of diverse environments, from extreme cold weather to high-intensity sports activities, ensuring durability, breathability, and optimal user experience.
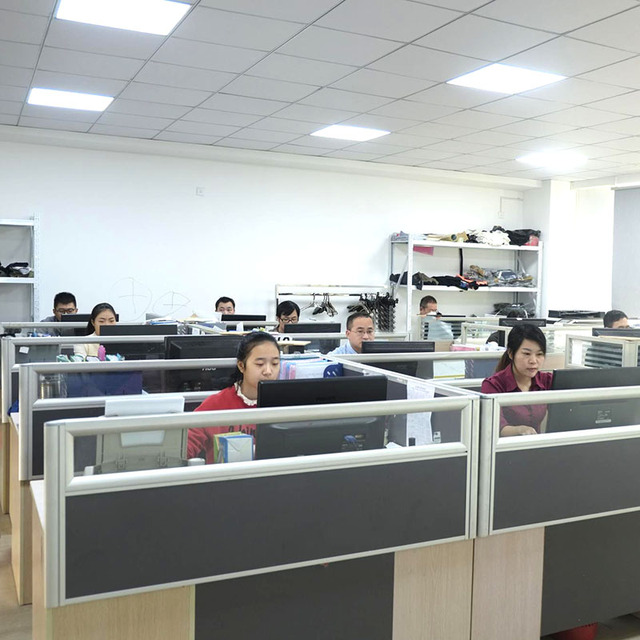
We provide comprehensive OEM and ODM services, enabling brands, distributors, and retailers to customize designs, materials, and branding according to their specific market needs. With strict quality control standards throughout every stage of production, we ensure consistency, reliability, and premium product quality.
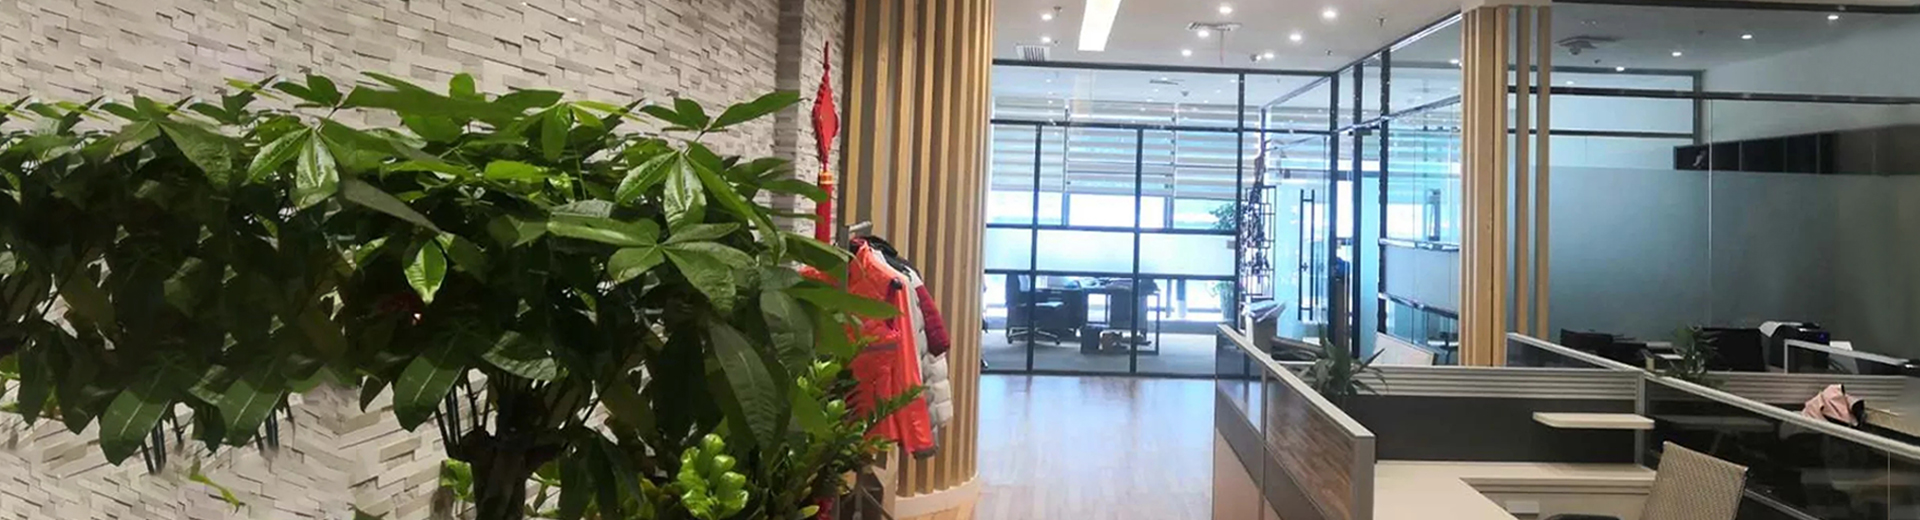
Serving clients worldwide, Guangzhou Lifted Clothe Co., Ltd. continues to expand its global presence by delivering stylish, functional, and performance-driven apparel. Our mission is to combine innovation and craftsmanship to support partners in building competitive and sustainable apparel brands in the international market.
Explore our complete export selection designed for kids, youth, men, and women serving the Grenville market.
Essential guidance on fabric selection, minimum order quantities, compliance, and international shipping.
We combine advanced 3D seamless knitting and 100% Merino wool fabric engineering with efficient Direct-to-Port logistics. Our team understands regional trade requirements in Grenville and offers customized duty-optimized documentation, flexible MOQs, and reliable quality guarantees.
100% Merino Wool (18.5 micron, 200-260 GSM) is ideal for low-temperature workwear, mountaineering, and extended multi-day wear due to its natural odor resistance and high thermal insulation. Synthetic polyester/spandex blends (180-220 GSM) excel in high-sweat, quick-dry, dynamic sports environments.
We provide full customization including jacquard woven waistbands, silicone anti-slip grippers, high-density heat-transfer reflective logos, custom color dyeing (Pantone matching), size customization (XS to 5XL+), and eco-friendly custom retail boxes.
Sample turnaround takes 7–14 business days. Bulk production is typically completed in 25–35 days upon tech-pack approval. Air express shipping takes 5–9 days, while sea freight door-to-door delivery typically ranges from 25–40 days depending on shipping lanes.
 Lifted Clothe